AkzoNobel
Chemical & CoatingsExplosion-Proof Paint Bucket Handling
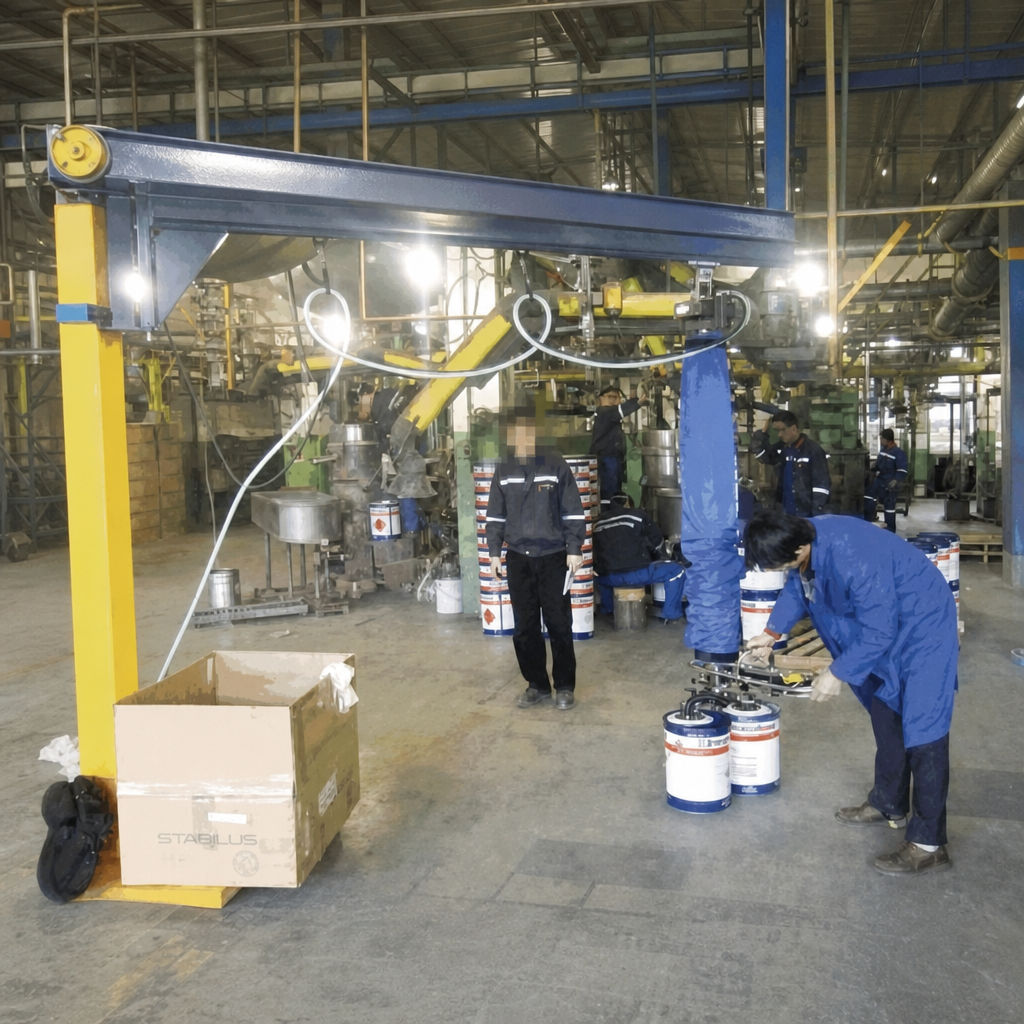
A pneumatic, explosion-proof lifting system moves one or two paint buckets from the filling line to the stacking area.
Browse case studies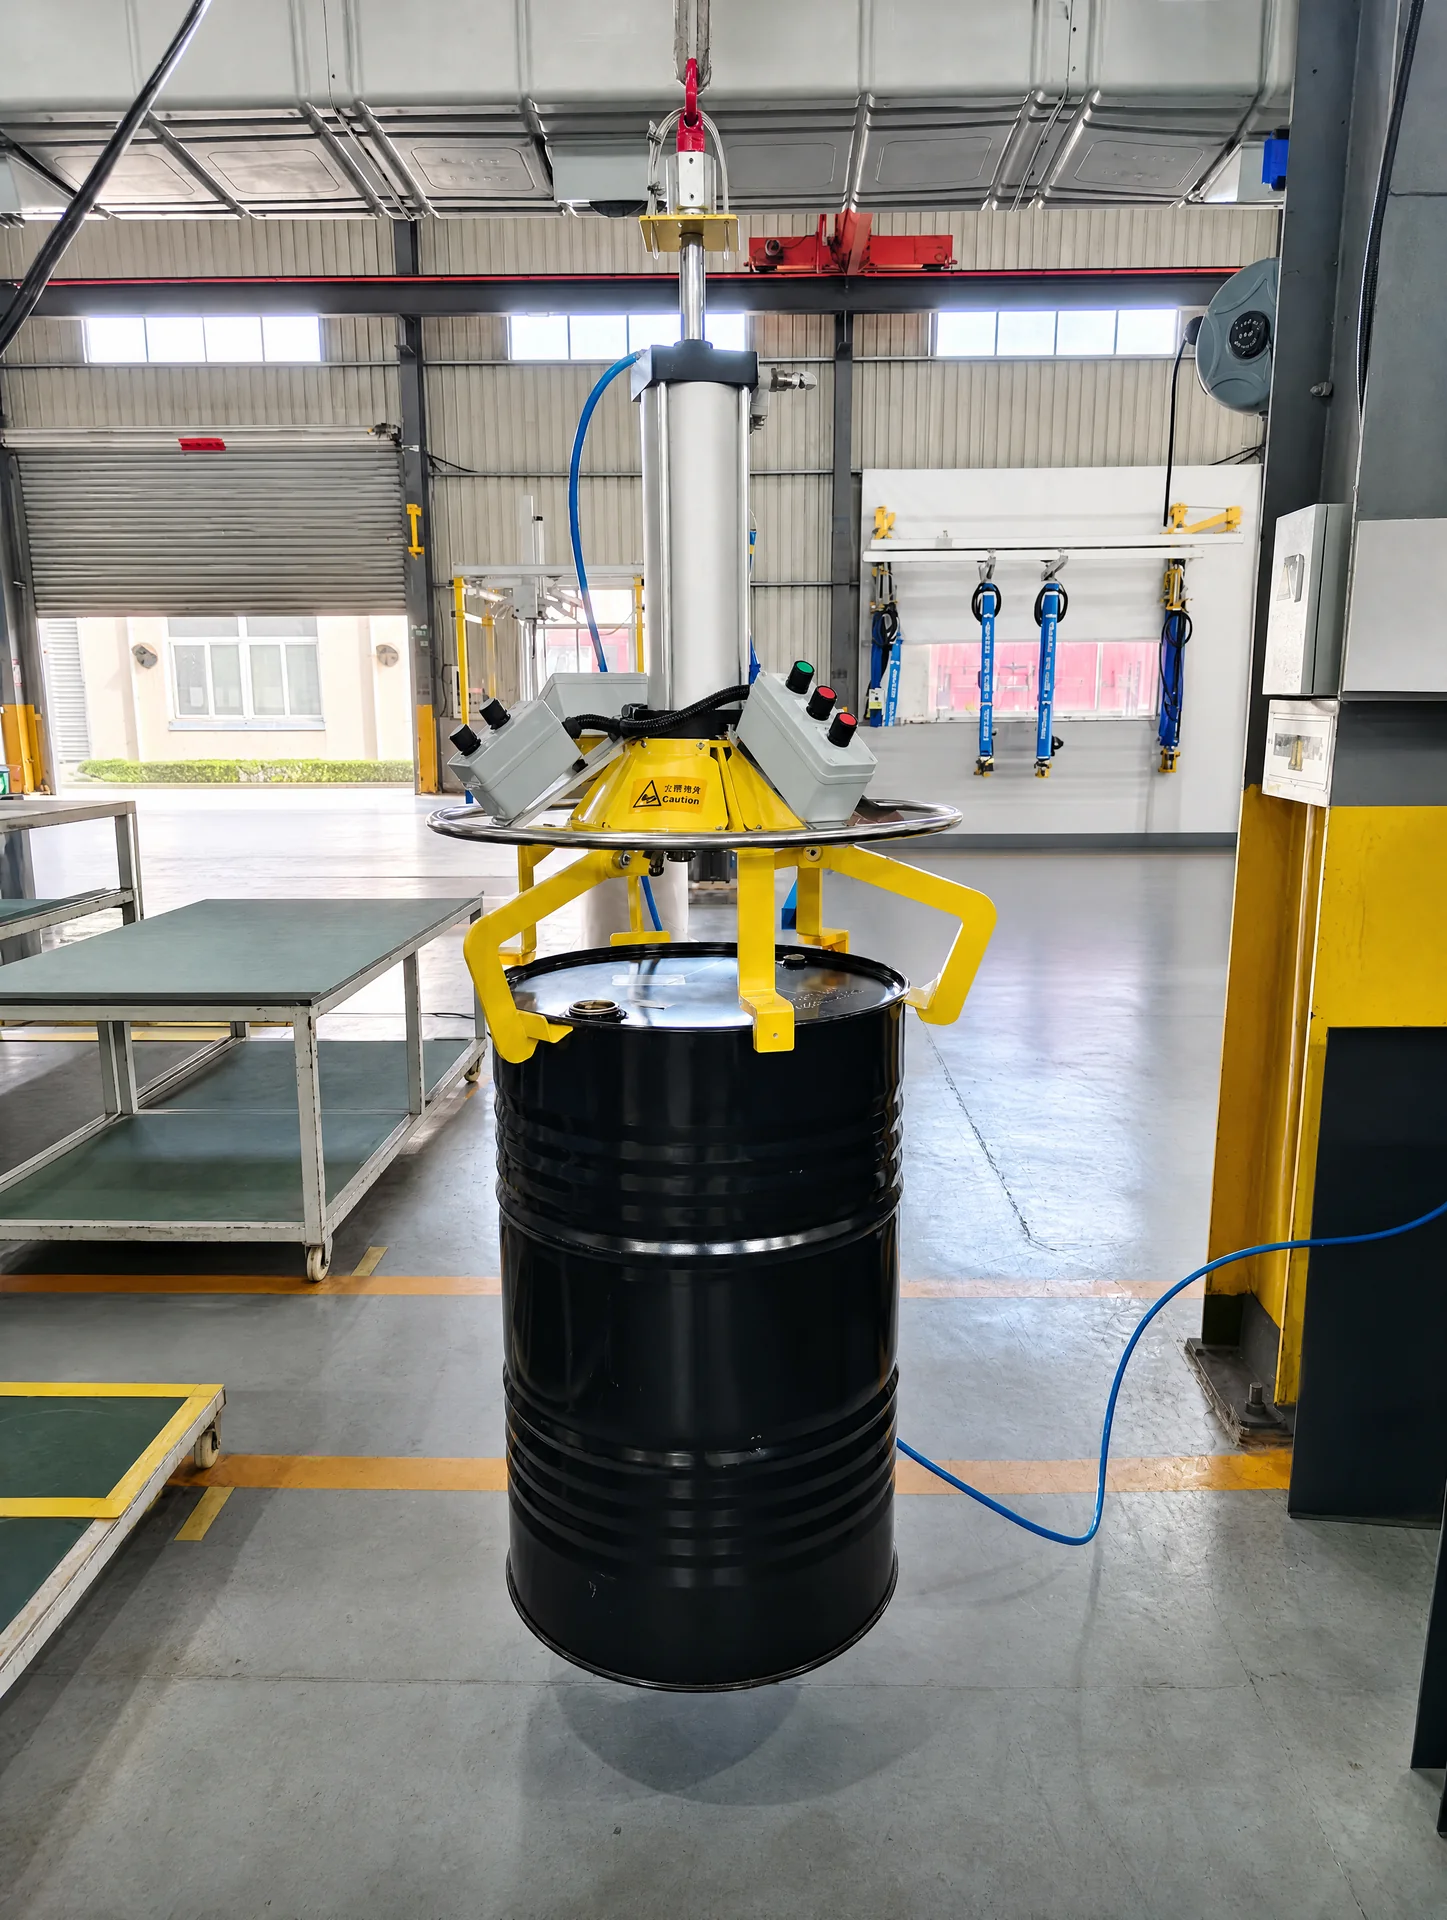
The chemical industry demands the highest standards of safety, precision, and reliability in material handling. HEROLIFT provides specialized lifting and handling solutions engineered to meet the rigorous requirements of chemical manufacturing and distribution environments. From steel and plastic drums to IBC totes, chemical sacks, and gas cylinders, our grippers, vacuum lifters, and powered trolleys enable operators to handle hazardous and heavy loads safely and efficiently - minimizing spill risks, reducing physical strain, and ensuring compliance with workplace safety regulations. By replacing manual drum handling and bulky forklifts with HEROLIFT's ergonomic, contamination-conscious systems, chemical plants can significantly reduce workplace injuries, protect product integrity, and maintain smooth, uninterrupted production workflows.
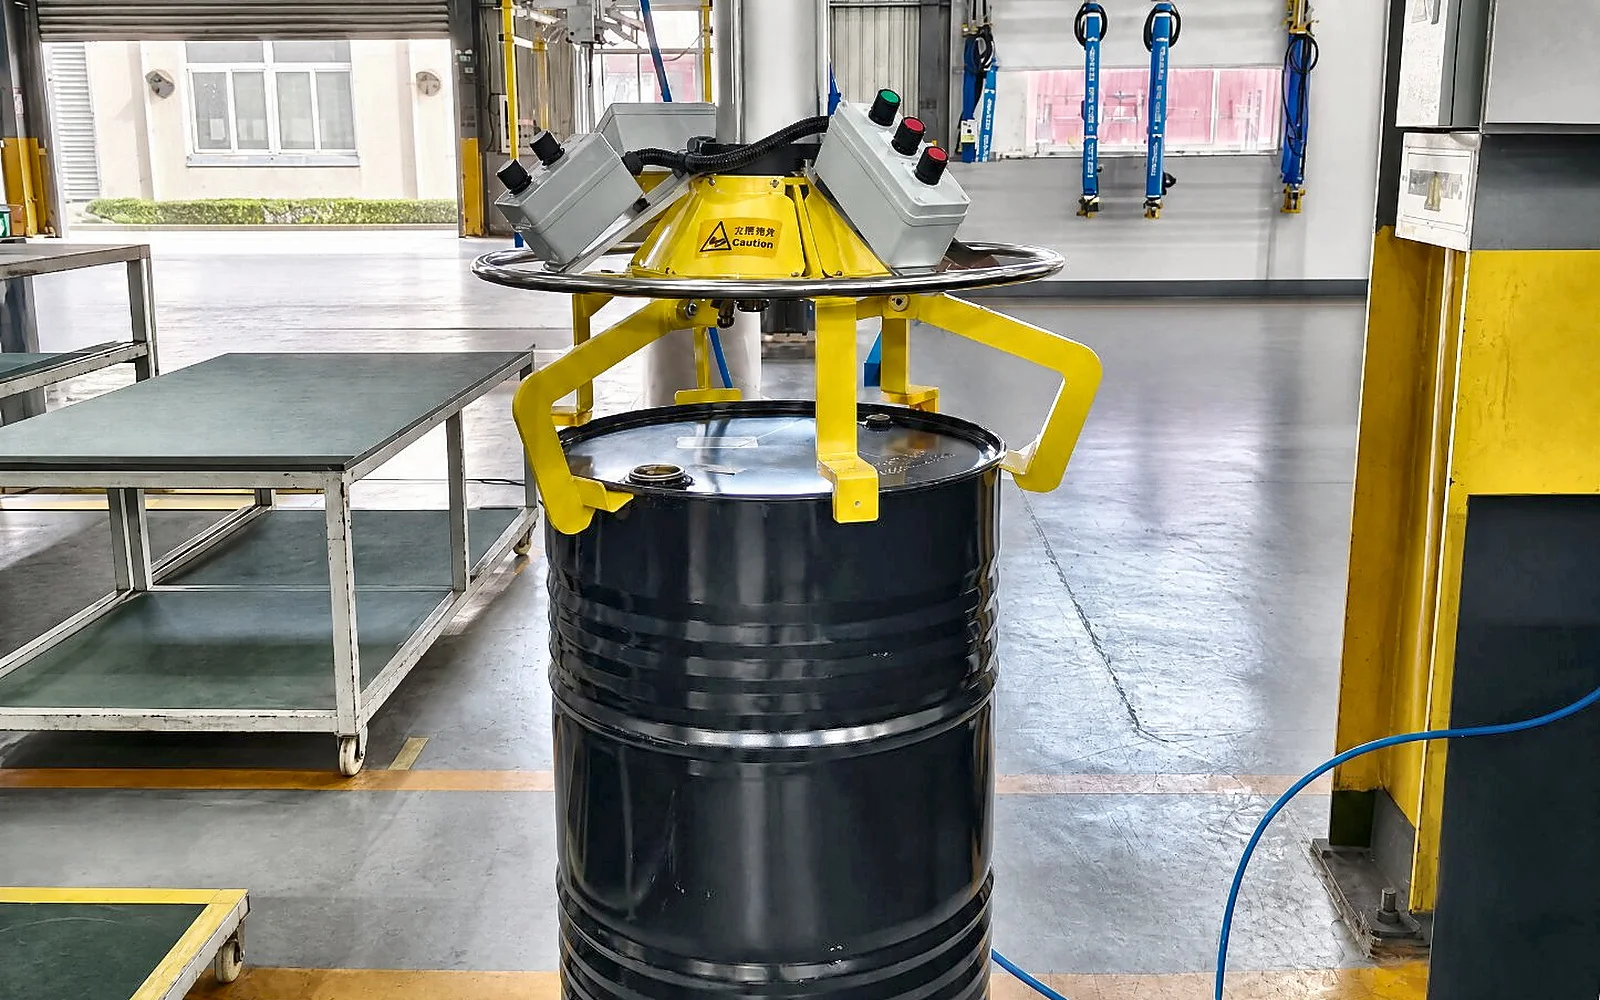
Herolift provides safe and compliant vacuum lifting and handling solutions. Intended for safe lifting and handling of chemicals, minimizing risks such as pollution, injury, and exposure to hazardous substances. Our stainless steel cleanroom lifters and explosion-proof series products are suitable for the harsh production environment of the chemical industry, supporting efficient material handling and reducing the pressure and safety hazards of operators.
Herolift provides vacuum lifting and trolley solutions that are suitable for various chemical scenarios, ensuring that you can easily handle any handling or transportation challenges. Our stainless steel solutions support material lifting in clean rooms or strictly controlled environments, and our explosion-proof series solutions are suitable for certain flammable or explosive environments. By using the Herolift lifting solution by operators to complete work, you can minimize the possibility of accidents, pollution, or exposure to toxic substances, ensuring safe and profitable operations.
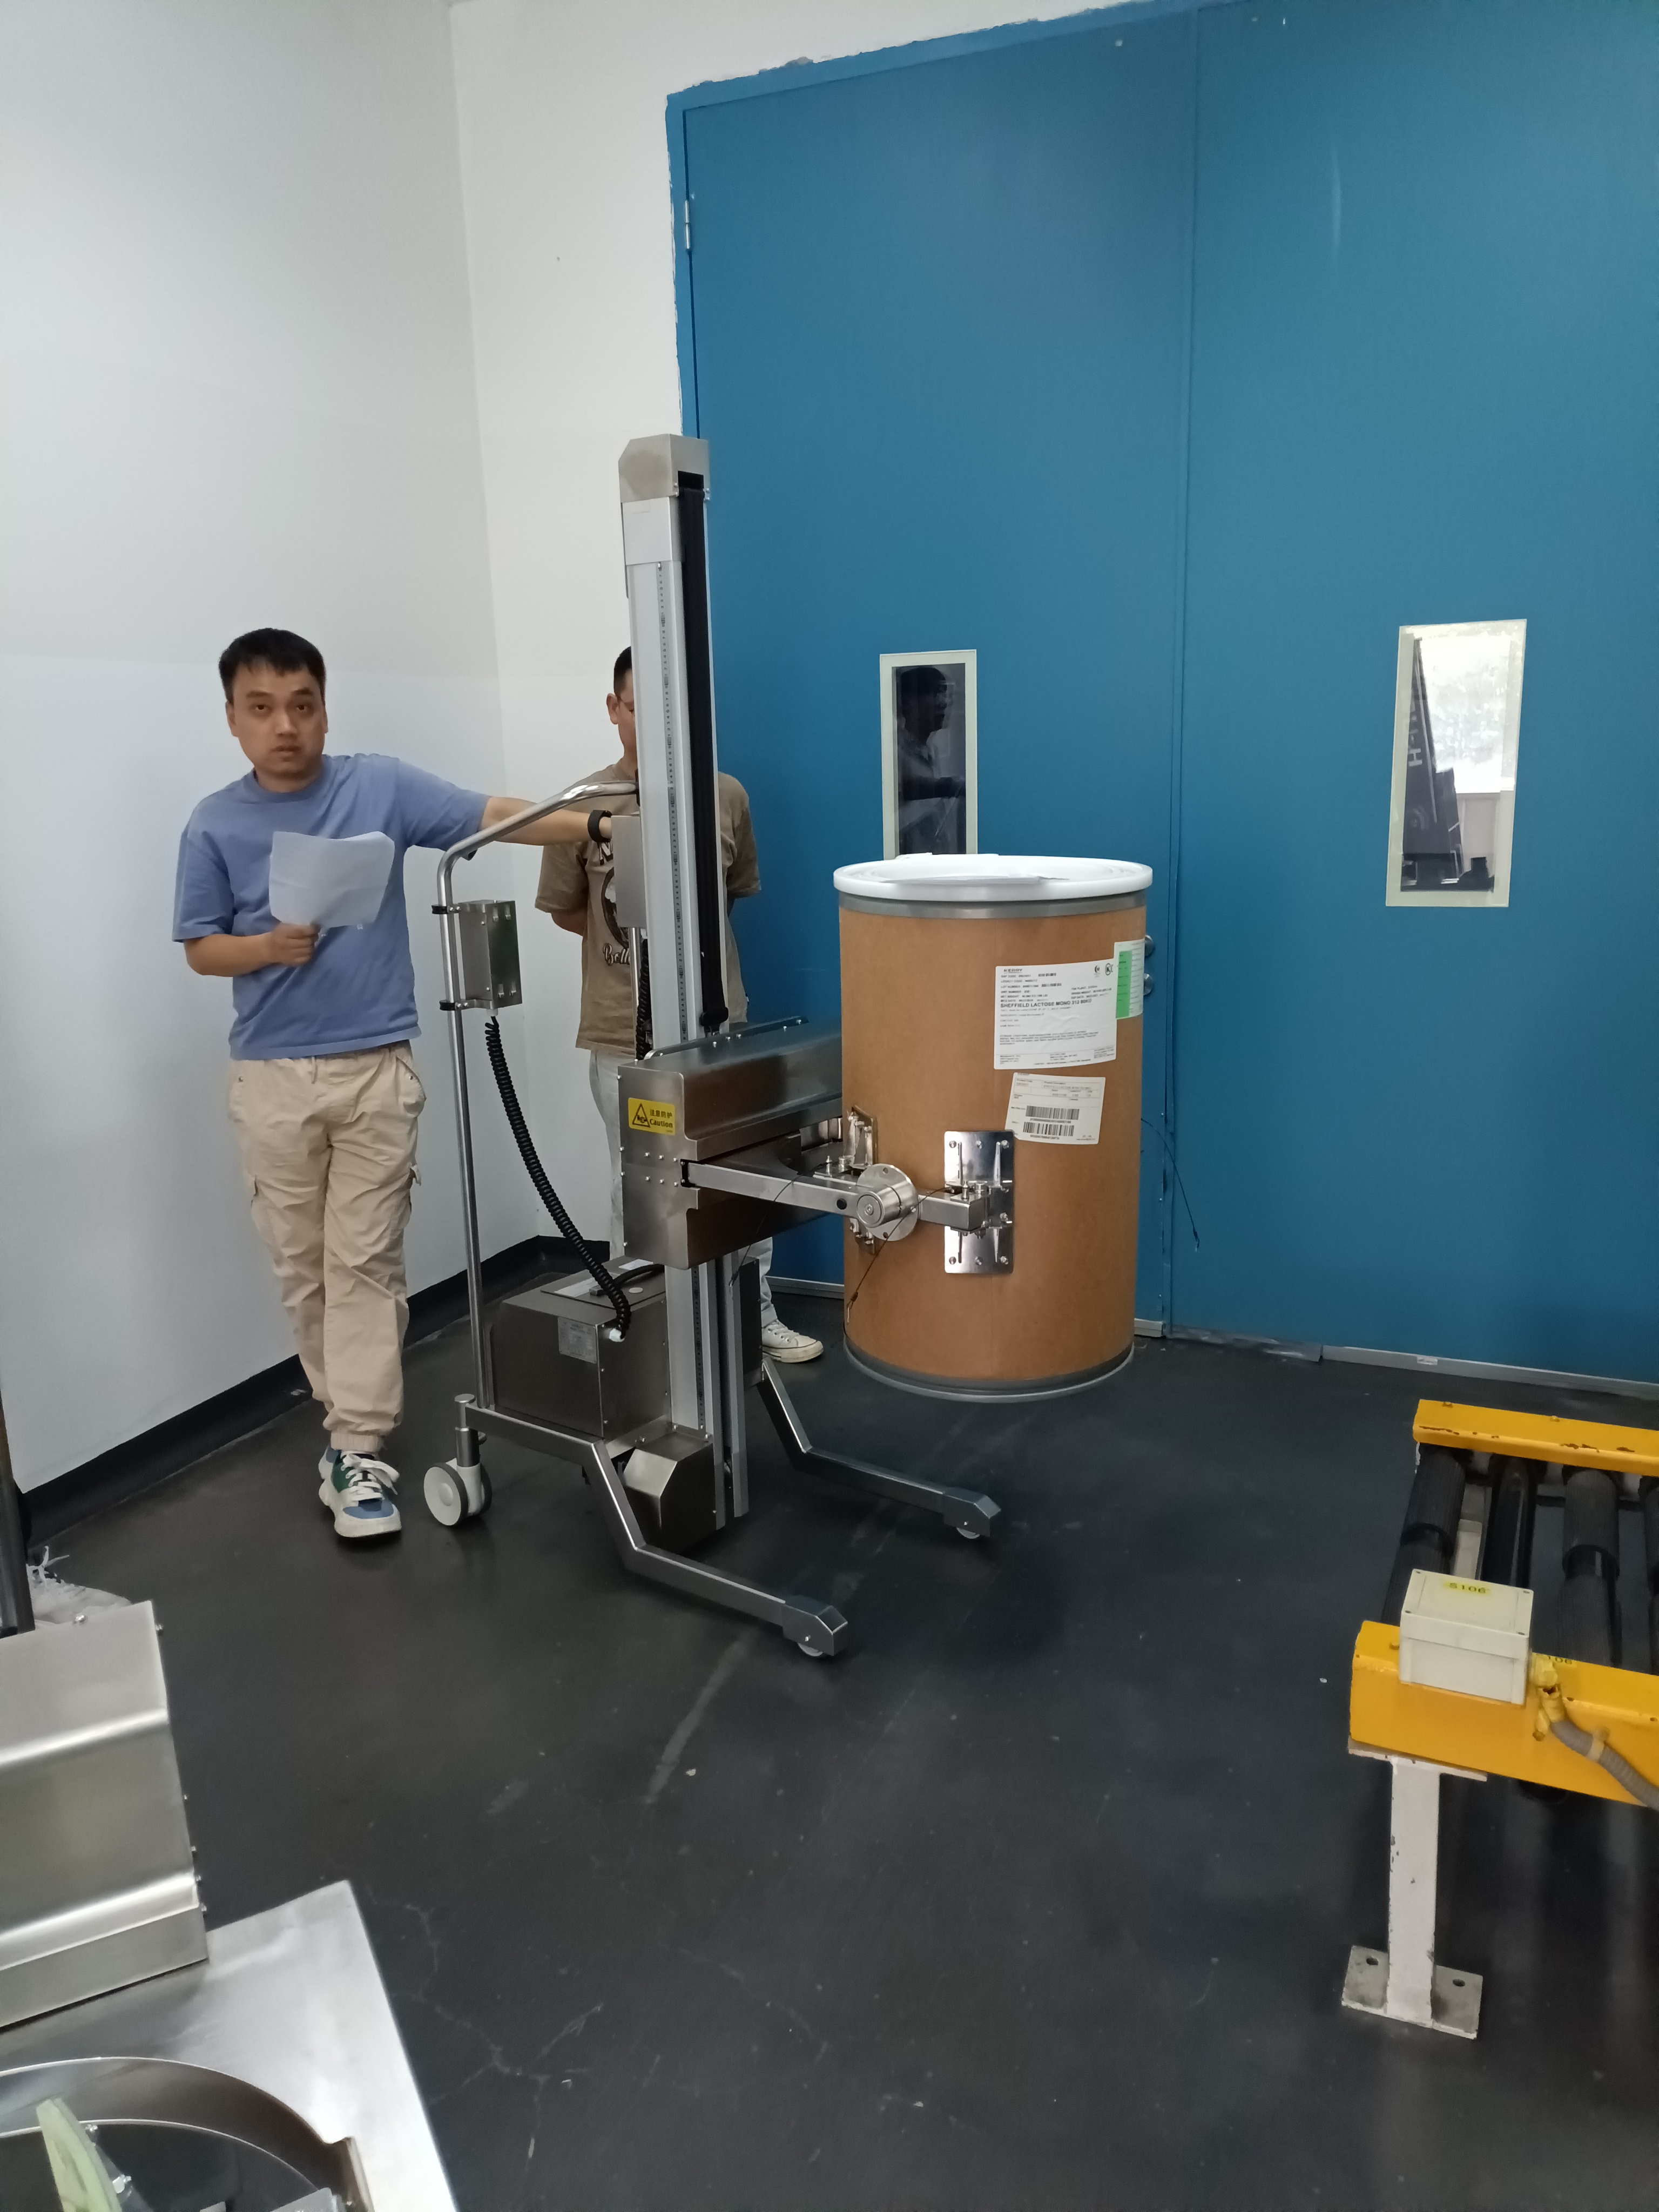
Herolift solutions can become the cornerstone of your highly secure and accurate lifting and handling system. By using Herolift vacuum lifters or drum lifters, chemical plants can maintain high standards of hygiene control while ensuring maximum efficiency and product preservation. Operators can easily lift, transport, rotate, tilt, or spin various materials such as drums, bags, and boxes to achieve high-precision and safe operations. In the past, palletizing was usually a manual and labor-intensive process. This has resulted in frequent repetitive stress injuries, downtime, and damage to products or ingredients. In addition, chemical products are highly flammable, which increases the risk of handling these products. Herolift's stainless steel lifters and drum lifters, as well as explosion-proof solutions, ensure the neatness and safety of any chemical pallets. Regardless of the number of employees, it is possible to pack or stack pallets more efficiently and quickly. Thus enhancing the diversity and flexibility of the workplace. Herolift has easy-to-use, easy to install and maintain equipment, making it the partner you need to achieve optimal growth and profits.
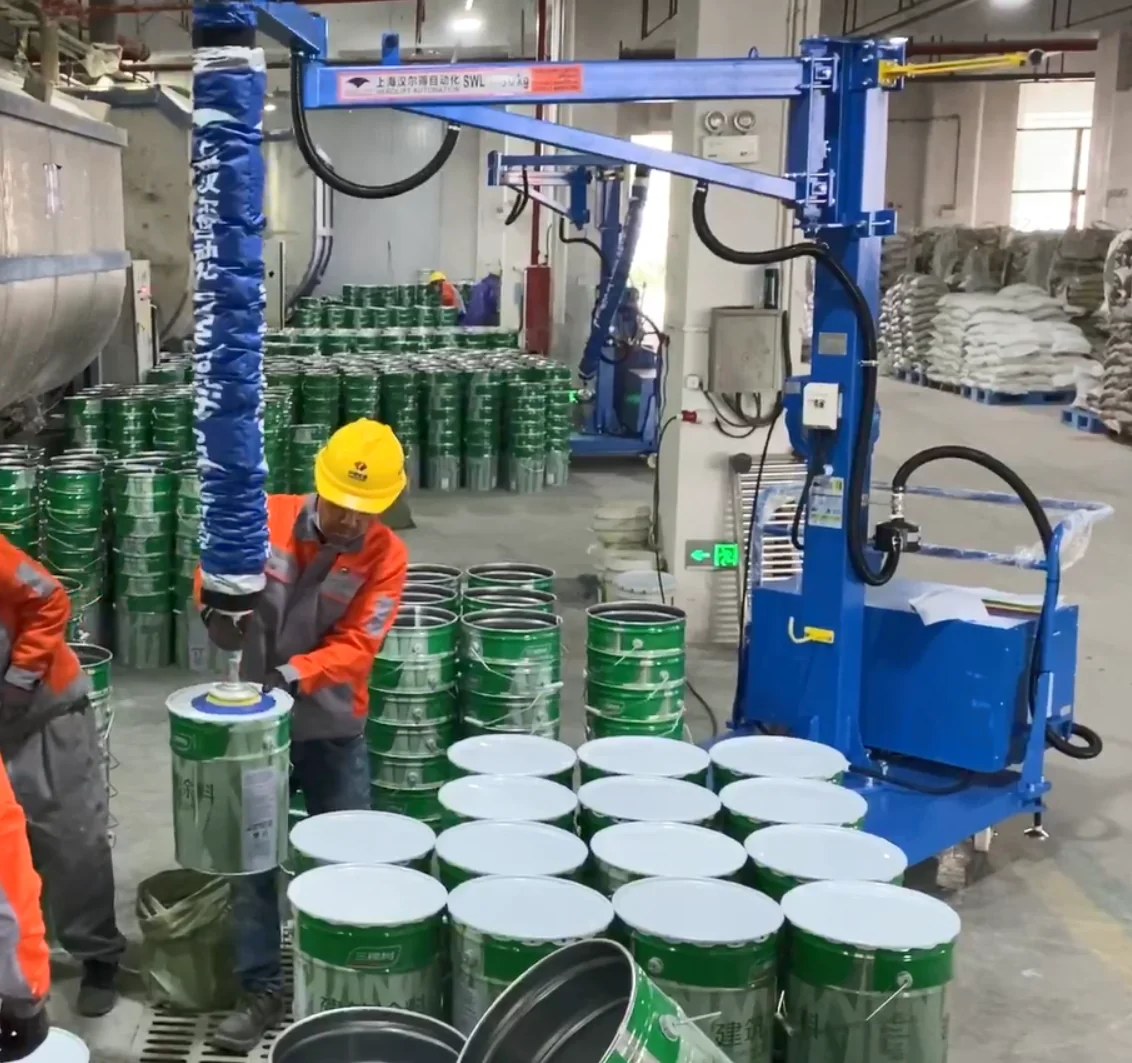
AkzoNobel
Chemical & CoatingsA pneumatic, explosion-proof lifting system moves one or two paint buckets from the filling line to the stacking area.
Browse case studies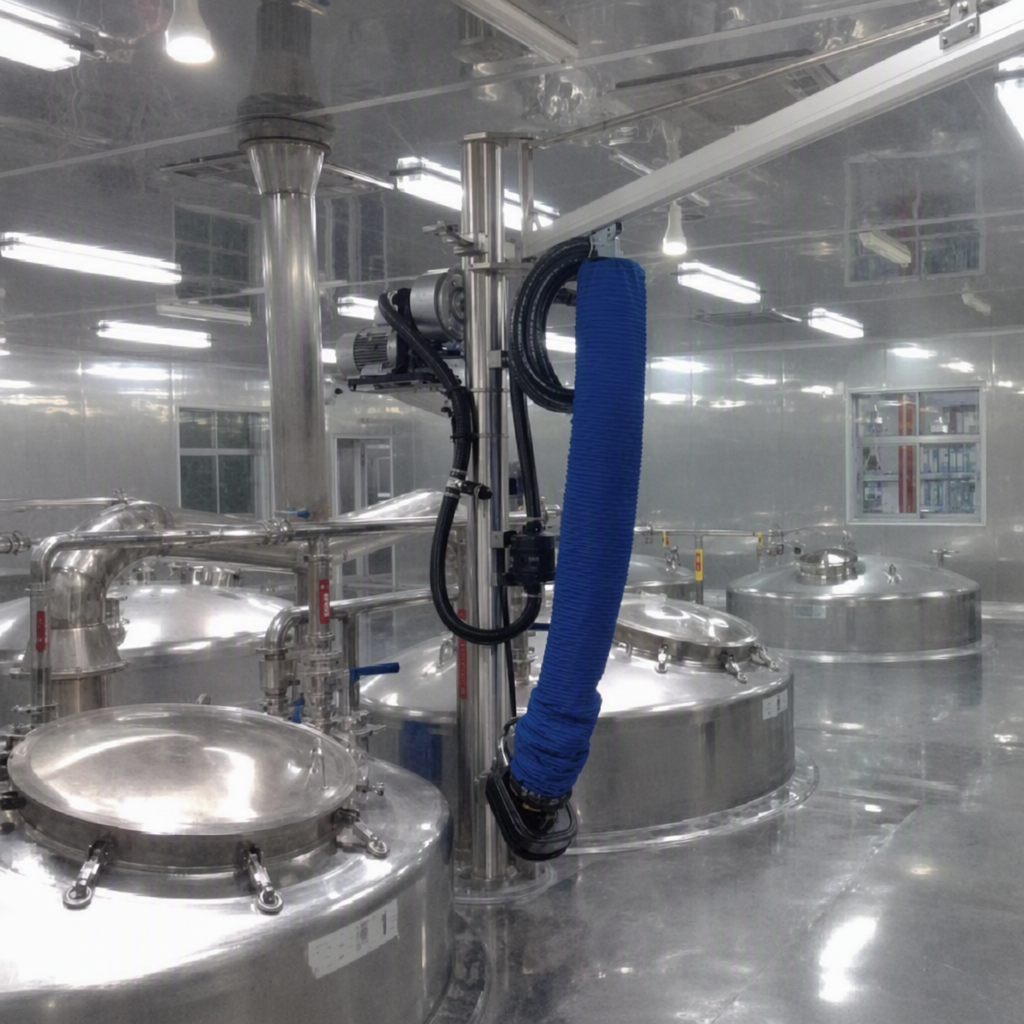
Red Bull
Food & BeverageA single operator unloads 50 kg sugar sacks and feeds production using a vacuum tube lifter with integrated grip-and-pour handling.
Browse case studies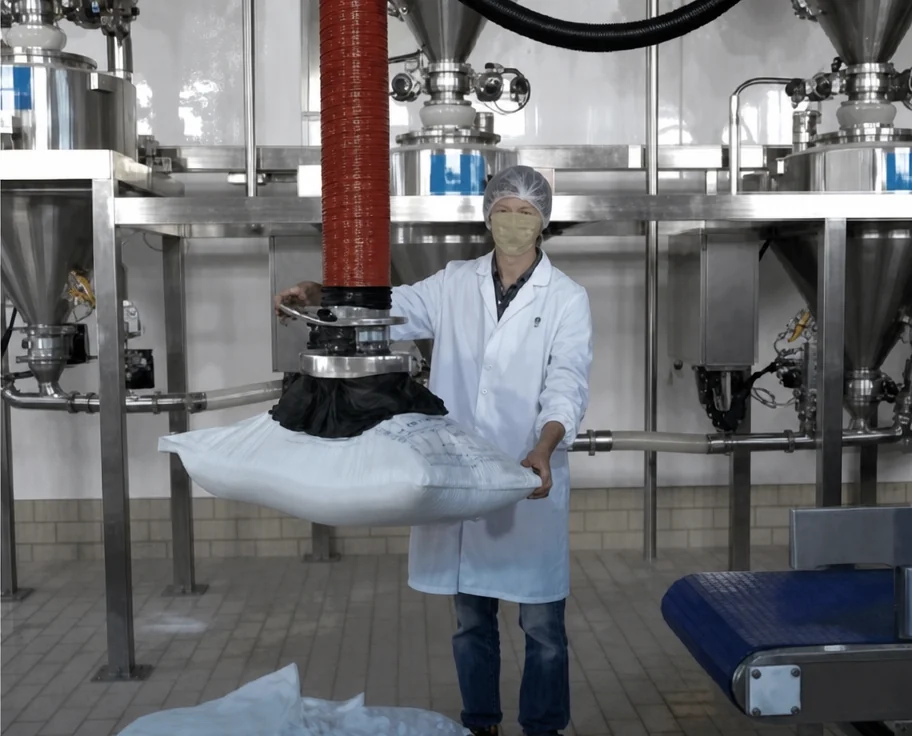
Yili Dairy
Dairy & FoodAn articulated lifting arm brings 50 kg sugar sack handling to a dairy workshop with restricted ceiling height.
Browse case studiesFAQ
The chemical industry requires safe handling of hazardous substances, with risks of pollution, injury, and exposure to toxic materials. Strict hygiene control and compliance with safety standards are essential.
Herolift provides stainless steel cleanroom lifters, explosion-proof series products, vacuum lifters, and drum lifters specifically designed for harsh chemical production environments .
Herolift solutions minimize the possibility of accidents, pollution, or exposure to toxic substances. The explosion-proof series is suitable for flammable or explosive environments. Operators can easily lift, transport, rotate, tilt, or spin various materials such as drums, bags, and boxes with high precision and safety .
Drums, bags, boxes, chemical pallets, and various containers commonly found in chemical plants.
Yes. Joe Greenley, a production leader in the chemical industry, said: “This is truly a blessing. By the end of the day, we were not even halfway to the exhaustion we felt before the Herolift equipment installation.”
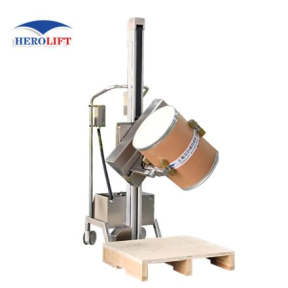 CT
Drum & Pail
Safe single-person drum dumping, moving, lifting, rotating, and emptying.
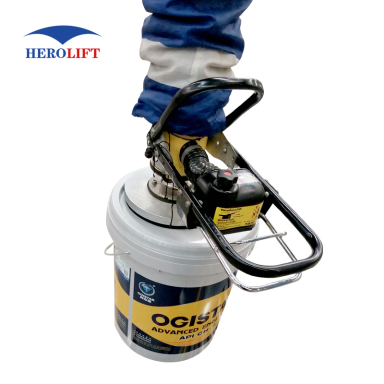 VEL-Drum
Drum & Pail
Ergonomic drum and pail handling with 360-degree rotation from pharma to food industry.
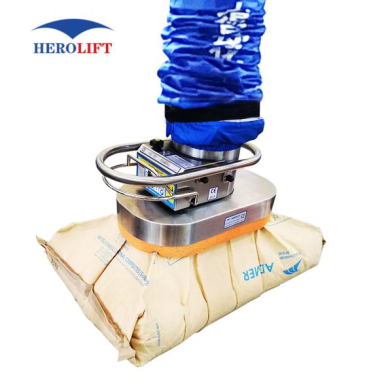 VEL-Bag
Bag & Sack
Safe and quick handling of all types of sacks, bags, and carton boxes.
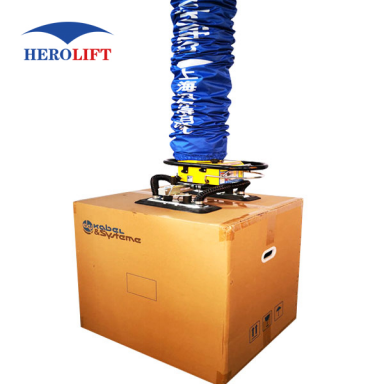 VEL-Box
Bag & Sack
Ergonomic all-in-one grip handle for carton boxes, wooden plates, sacks, and drums.
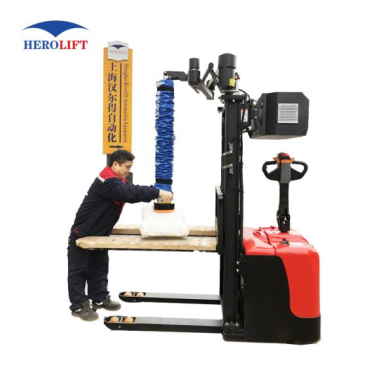 VEL-MP
Bag & Sack
Mobile order-picking vacuum lifter integrated with stacker for warehouse operations.
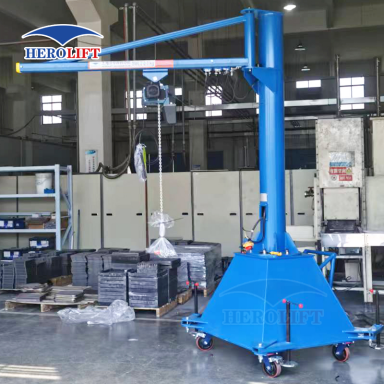 RA
Automation
Mobile jib crane for flexible, all-direction production line lifting up to 2000 kg.